How to Remove PET Silicone Tape After Powder Coating
Technical Insights · Powder Coating
How to Remove PET Silicone Tape After Powder Coating
To remove PET silicone tape after powder coating, use the removal condition, peel direction, support method and inspection criteria proven on the actual part and coating cycle. A controlled low-angle peel can protect the coating edge, but the correct moment must be established by trials rather than guessed from oven setpoint or tape color.

Quick Answer
Unmasking is a controlled finishing operation, not a cleanup task left to operator preference. Define which coating edge is acceptable, when the part may be handled, where peeling starts, how the panel is supported, and how removed tape is accounted for. If the mask fractures, leaves adhesive, pulls coating from the intended boundary, or exposes the wrong area, stop and separate the defect cause before changing tape or peel force.
Define the Removal Window
The usable window begins only after the part reaches the released handling condition and ends before time, temperature or storage increases the chance of difficult removal. This condition can differ between thin sheet, castings, welded assemblies and heavy inserts because they cool at different rates. The coating also changes from soft to increasingly resistant to edge fracture as it cools. The process owner should therefore base the instruction on part condition and measured evidence, not a fixed assumption applied to every rack position.
Document whether masking is removed on the line, at a dedicated station or after temporary storage. Include repeated cure passes, line stops, rework cycles and the longest approved delay. If operators receive mixed part temperatures, provide an objective release method such as a qualified wait rule, contact-free measurement or fixture sequence owned by the finishing team.
| Process factor | Question to answer | Why it matters |
|---|---|---|
| Part condition | What handling temperature or time state permits safe support? | Protects operators and prevents distortion or marking |
| Coating state | Can the edge release without smearing, stretching or chipping? | Controls boundary quality |
| Removal delay | What is the normal and maximum approved delay? | Captures adhesion change and production interruptions |
| Geometry | Where can the peel begin and where must the part be supported? | Reduces bending and uncontrolled edge loading |
| Downstream use | Will the exposed land be bonded, grounded, sealed or assembled? | Defines cleanliness and dimensional acceptance |
Prepare the Part and Removal Station
Confirm identity and orientation
Match the part, coating recipe, mask drawing and work instruction before touching the tape. Similar housings can have different no-coat lands. Use the released datum or image standard to confirm that the correct boundary was masked and that all pull tabs are present.
Support the panel near the peel line
A large door or thin panel can flex while tape is removed. Support the part so peel load does not bend a flange, twist a welded corner or lever against fresh coating. Keep gloves, bench pads and fixtures clean enough for the specified cosmetic and functional surfaces.
Plan tape and fragment accountability
Decide how complete strips, die-cut rings, plugs and small tabs are counted or visually confirmed. A missing fragment can remain in a thread, vent, drain, gasket path or bonding land. The removal station needs suitable lighting and a defined container for used masking material.
| Mask format | Preferred preparation | Primary removal risk |
|---|---|---|
| Long straight strip | Accessible tab and continuous support | High peel load or coating-edge bridging |
| Die-cut patch | Nonadhesive tab and defined pull direction | Torn corner or incomplete accounting |
| Ring or frame | Split point that avoids the critical land | Stretching across a corner or leaving a segment |
| Multiple small pieces | Piece-count standard or carrier map | One mask remains on the part |
| Overlapped strips | Released removal order for every joint | One layer traps another or chips the edge |
Use a Controlled Peel Method
Start from the designed tab rather than digging under the coating boundary with an unapproved blade. Fold the tape back on itself and peel progressively at the approved angle and direction while supporting the part close to the moving line. Maintain a steady motion; sharp jerks can concentrate load, while an uncontrolled upward pull can lift the coating edge or flex the workpiece.
Follow corners in the sequence proven during qualification. For a ring or perimeter mask, a short rotation of the part may be safer than pulling across the opening. Do not add heat, solvent, abrasive tools or adhesive remover unless the finishing and downstream assembly owners have released that method for the exact surface.
Recommended Unmasking Workflow
- Verify the traveler. Confirm part revision, powder, cycle, mask drawing and required status.
- Check handling condition. Apply the approved safety and process release rule before contact.
- Inspect before removal. Record obvious lift, powder bridges, tears or missing tabs.
- Support the part. Place the panel or housing on the qualified clean fixture.
- Start at the pull tab. Avoid sharp tools at the coating boundary.
- Peel in the released direction. Keep the angle and speed controlled around corners and joints.
- Account for every piece. Compare removed material with the drawing or piece-count standard.
- Inspect the exposed land. Check coating edge, dimensions, residue, fragments and surface damage.
- Segregate defects. Preserve evidence before cleaning, touching up or remasking.
- Complete functional checks. Perform the specified fit, bond, seal, continuity or assembly verification.
Validate Removal on Production Parts
Use representative metals, pretreatments, powders, film builds, geometry, rack positions, thermal masses and operators. Include the shortest and longest approved removal delays and credible line interruptions. Coupons can screen adhesive transfer, but they do not reproduce a formed corner, weld, textured land, deep recess or flexible door.
| Validation group | What to observe | Release evidence |
|---|---|---|
| Removal effort | Start, steady peel, corners, joints and operator access | Repeatable method without unsafe force |
| Coating edge | Chips, tearing, bridges, burrs and exposed width | Drawing and approved appearance standard |
| Tape condition | Tears, adhesive transfer, shrinkage and missing pieces | Complete removal and fragment accountability |
| Exposed surface | Residue, staining, powder creep and physical damage | Released cleanliness and dimensional check |
| Final function | Bonding, sealing, grounding, fastening, fit or corrosion plan | Product-owner acceptance tests |
Diagnose Defects Before Changing the Tape
Coating chips can originate from powder bridging over the tape edge, excessive film build, an unsuitable boundary geometry, a burr, removal direction or the selected removal condition. Adhesive transfer can involve surface contamination, the exact adhesive, thermal exposure, repeated passes or excessive delay. Tape tearing can involve a sharp coating ridge, weak tab design, a nicked edge or an inaccessible peel path.
Do not treat every defect as insufficient heat resistance or solve it automatically with stronger adhesion. First compare rack position, part temperature record, powder build, mask placement, application pressure and removal timing. Change one controlled variable, repeat the relevant trial and update the work instruction only after the complete part passes.
Related Products and Articles
Frequently Asked Questions
Should PET silicone tape be removed while the part is hot?
Not by a universal rule. Establish a safe, repeatable condition on the actual part and coating cycle. Operator safety, coating state, thermal mass, adhesive response and the downstream surface all matter.
What peel angle prevents coating damage?
A low, controlled peel is often screened because it can reduce upward loading, but the released angle and direction must be proven on the real geometry and coating edge.
Can solvent be used to remove adhesive residue?
Only if the finishing and downstream process owners approve it for the exact coating and exposed surface. An unqualified solvent can alter appearance, bonding, sealing or corrosion performance.
Why does tape remove cleanly from one rack position but not another?
Part temperature, film build, spray access, thermal mass, dwell, contamination and removal delay may differ across the rack. Compare process records before blaming the tape lot.
What information belongs in a removal trial request?
Provide metal and pretreatment, powder, measured cycle, geometry, mask drawing, tape format, application method, removal timing, acceptable edge, exposed-surface function and inspection plan.
Build a Controlled PET Tape Removal Trial
Share the part drawing, coating-free boundary, metal and pretreatment, powder system, measured cure history, tape format, expected removal condition, handling fixture, downstream function and acceptance tests. JIAO TAO TAO can prepare slit or die-cut PET silicone tape samples for a documented line evaluation.
Discuss PET tape removal after powder coating
Polyimide Tape for PCB Underfill Dam Masking
Related Article
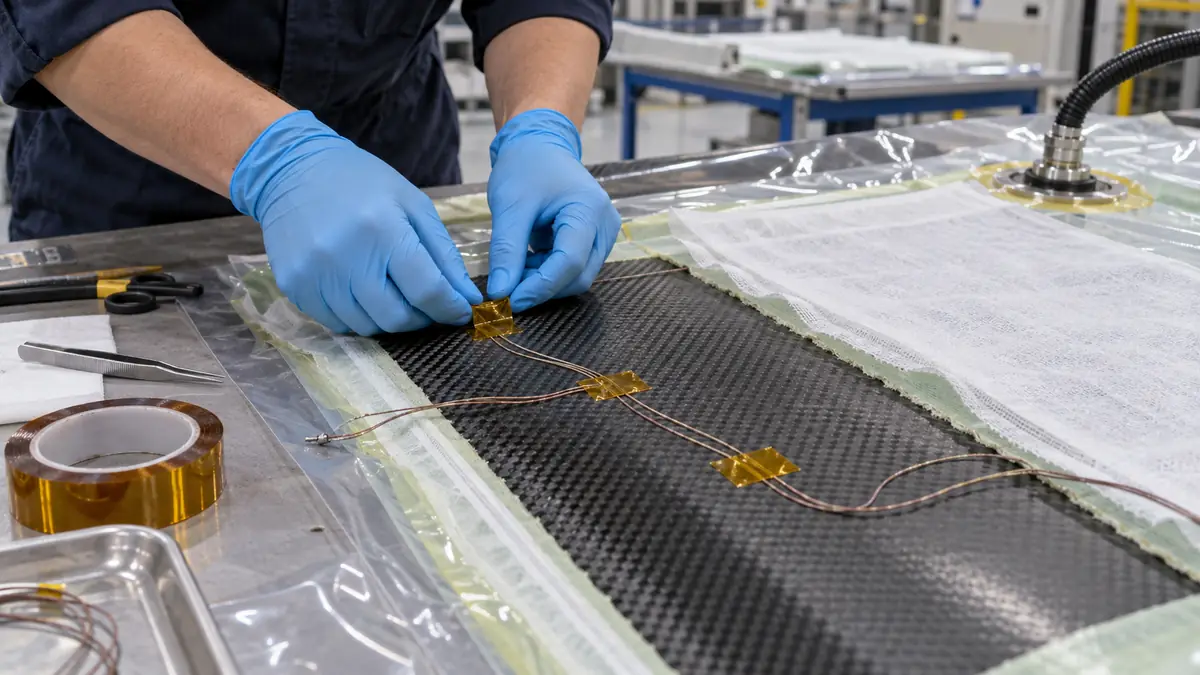
Need help choosing the right industrial tape?
Send us your application details, including temperature, surface material, size, quantity and current problem. Our team will help recommend a suitable tape material or custom die-cut solution.
simon@jiaotaotao.com
+86-136 1277 5969
+86-136 1277 5969
