PTFE Tape for Composite Tool Flange Release Surfaces
Technical Insights · Composite Tooling
PTFE Tape for Composite Tool Flange Release Surfaces
PTFE tape for composite tool flange release surfaces can create a replaceable low-stick zone outside the mold cavity where sealant tape, resin squeeze-out, bagging films, and consumables may contact the tooling. The construction, flange geometry, cure cycle, vacuum-bag stack, and cleanup method must be qualified together without changing the molded surface or vacuum integrity.

Quick Answer
Use adhesive-backed PTFE film or PTFE-coated fiberglass tape only on a tool-flange location approved by the composite process owner. Keep it outside the mold cavity, datum surfaces, vacuum ports, thermocouple paths, sealant lands, and other controlled features unless the released process explicitly includes the tape there. Define the tape as a service layer, not as a universal mold release or a repair for damaged tooling.
Define the Approved Tool-Flange Zone
A composite mold flange may support vacuum-bag sealant, breather extensions, pleats, thermocouple leads, resin dams, edge trim, locating features, or handling hardware. Some areas need a clean bare tool surface for sealant adhesion; others may benefit from a replaceable PTFE release strip where resin or adhesive contamination is expected. Mark those zones on the tooling or process drawing before selecting tape.
Measure the available flat width, inside and outside radii, bolt holes, vacuum channels, port locations, and distance from the mold cavity. A tape edge too close to the cavity can print into the laminate or create a resin path. An edge under sealant tape can change vacuum sealing. A strip placed over a port or datum can block a function even when it looks neatly installed.
| Tooling input | What to document | Why it matters |
|---|---|---|
| Flange function | Sealant land, bag support, resin catch, trim allowance, or service zone | Determines whether PTFE tape belongs there |
| Tool material | Metal, composite, coated tool, finish, repair history, and release system | Controls adhesion and removal risk |
| Geometry | Flat width, radii, corners, holes, grooves, ports, and cavity distance | Defines practical width and seam layout |
| Cure exposure | Temperature, ramp, dwell, pressure or vacuum, number of cycles, and cooldown | Represents thermal and mechanical stress |
| Consumables | Resin, release film, peel ply, breather, bag film, sealant, and cleaners | Identifies contact and compatibility risks |
Compare PTFE Tape Constructions
PTFE film adhesive tape
Skived or extruded PTFE film tape can provide a smooth, relatively thin release face. It may suit flat controlled zones where surface texture must be minimized. The film can be vulnerable to puncture, edge curl, or tearing at a sharp tool feature. Thickness, adhesive support, and cut-edge quality must be matched to the flange.
PTFE-coated fiberglass tape
PTFE-coated fiberglass adds woven reinforcement and dimensional support during application. It can handle broader strips and repeated service more robustly, but the weave, thickness, stiffness, and overlap may leave an impression in pressure-sensitive consumables. It is not automatically the best choice close to the laminate edge.
Converted strips and profiles
A converted profile can control width, holes, corner reliefs, port clearances, and liner tabs. It can also reduce ragged hand cuts and mixed seam positions. The drawing should specify which face receives the tape, how the part is oriented, and whether the strip is replaced every cure, after a condition limit, or at a planned interval.
| Construction | Potential advantage | Main qualification concern |
|---|---|---|
| PTFE film tape | Smooth, thin release face on flat flange areas | Puncture, edge curl, cold flow, and adhesive exposure |
| PTFE-coated fiberglass tape | Reinforcement and easier handling of wider strips | Weave texture, seam height, stiffness, and marking |
| Zone or differential-adhesive tape | Adhesive limited to controlled support areas | Correct orientation and compatibility with the tool design |
| Converted flange profile | Repeatable holes, radii, widths, and liner features | Drawing control, tolerance, presentation, and replacement supply |
| Permanent tool coating | Engineered long-term release surface where approved | Repair, recoating, cure compatibility, and downtime |
Design Seams, Corners, and Replacement Access
Use the fewest joints practical. A butt joint avoids a double-thickness ridge but can open under thermal cycling. An overlap is easier to keep continuous but creates a step that may trap resin, print into a consumable stack, or interfere with a sealant line. Place the joint outside critical vacuum and laminate paths and document its orientation.
Do not stretch PTFE tape around a corner. Stored tension can lift the inside or outside edge during heat-up. Use a broader radius, relief cut, separate controlled pieces, or a converted corner profile. Keep every edge supported on sound tooling and provide removal access that does not require a metal scraper against the mold surface.
Controlled Installation Workflow
- Approve the location. Review the tool and layup documents, cavity edge, vacuum path, and service zone.
- Inspect the tool. Check coating damage, chips, resin, sealant, dents, ports, and previous adhesive.
- Prepare by the released method. Use only cleaners and wipes approved for the tool surface.
- Cut or select the profile. Verify width, holes, reliefs, liner, and orientation before exposing adhesive.
- Align from a datum. Maintain the specified distance from the cavity and sealant lands.
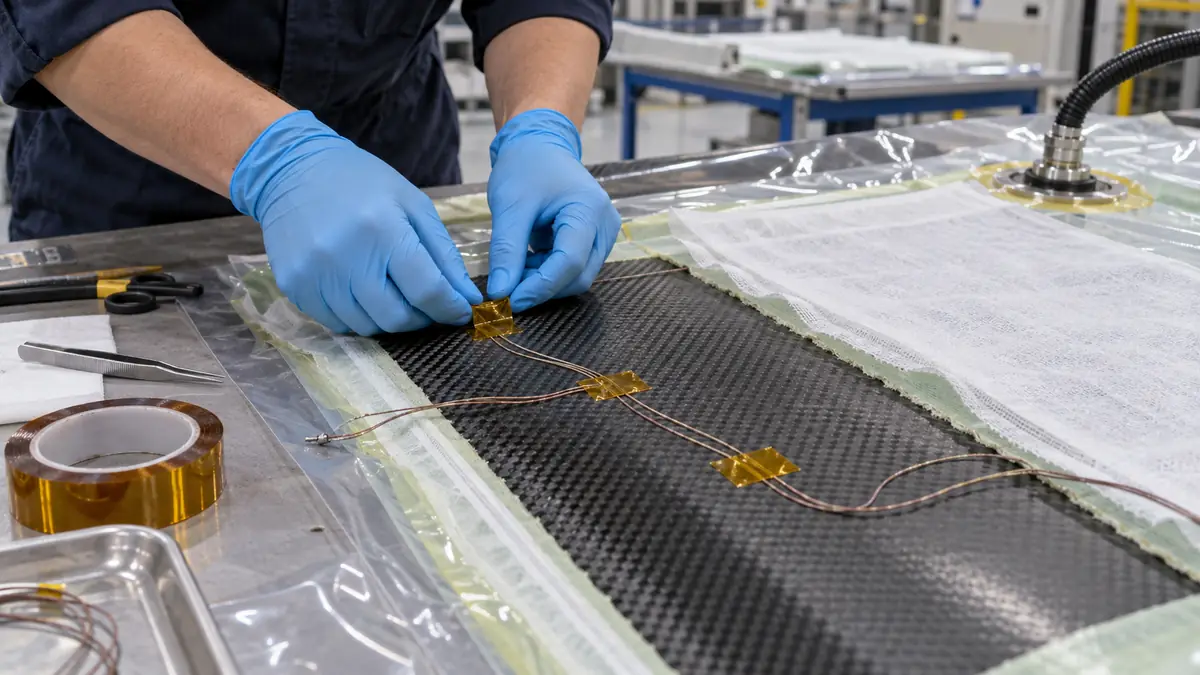
- Apply without stretch. Smooth progressively and avoid wrinkles, bubbles, and trapped debris.
- Roll the full bond area. Use controlled pressure without damaging the tool or tape surface.
- Inspect seams and ports. Confirm edges, joints, vacuum access, and consumable clearances.
- Run the representative cure. Include actual layup, bagging, vacuum, pressure, temperature, and cooling.
- Inspect and record wear. Check release, resin buildup, lift, residue, laminate edge, and tool condition.
Validate Release, Vacuum Integrity, and Part Quality
Evaluate the tape on the actual tool or a production-representative flange coupon with the real release system, resin, consumables, sealant, cleaner, vacuum level, pressure method, thermal cycle, and removal stage. Include repeated cycles if the intended service interval is longer than one cure. A room-temperature peel test cannot reproduce autoclave or oven cycling, resin flow, vacuum stress, and cleanup.
| Validation group | What to observe | Release question |
|---|---|---|
| Installation | Position, full contact, wrinkles, seams, port clearance, and surface cleanliness | Can technicians reproduce the layout? |
| Vacuum and cure | Leak rate, sealant contact, lift, bubbles, resin tracks, and thermal movement | Does the process remain within its released window? |
| Part quality | Laminate edge, flash, marks, thickness, trim allowance, and contamination | Is the finished part unaffected? |
| Release and cleanup | Bag removal, sealant pickup, resin release, scraping need, and residue | Does the layer simplify service without tool damage? |
| Durability | Cuts, glazing, fray, edge lift, discoloration, adhesive transfer, and cycle count | Are replacement limits visible and repeatable? |
Troubleshoot Tool-Flange Tape Problems
A vacuum leak after installation can involve tape crossing a sealant land, a lifted edge beneath the bag, a blocked port, debris, or an unrelated bagging defect. Resin beneath the tape can enter through a seam, cut edge, puncture, or unsupported contour. Wrinkles and bubbles often trace to rushed placement, a contaminated tool, excessive tape width, or stretching around a radius.
If adhesive transfers to the tool, compare the exact construction, surface finish, cleaner, cure history, cycle count, cooldown, and peel method. Do not scrape aggressively or introduce an unapproved solvent. Stop and follow the tooling owner's repair and cleaning procedure. Tape should never hide coating loss, cracks, porosity, or geometry damage.
↑ Back to contentsRelated Products and Articles
Frequently Asked Questions
Can PTFE tape replace mold release on a composite tool?
No. It can be evaluated as a local service layer on an approved flange zone, but the process owner must define the mold-cavity release system and complete qualified layup.
Should PTFE tape sit under vacuum-bag sealant?
Only when the released process specifically qualifies that interface. A low-stick or textured layer can change sealant adhesion and vacuum performance.
Is PTFE film or PTFE-coated fiberglass better?
Film offers a smoother, thinner face; coated fiberglass adds reinforcement. Tool geometry, marking sensitivity, cure exposure, wear, and seam design determine the better trial candidate.
How often should flange tape be replaced?
Set condition-based limits for cuts, lift, resin buildup, fray, glazing, residue, seam movement, and vacuum or part-quality changes, supported by cycle records.
What information belongs in an RFQ?
Provide the tool material and finish, flange drawing, approved tape zone, cure profile, vacuum or pressure method, resin and consumables, cleaner, seam limits, service interval, and acceptance criteria.
Define a Composite Tool-Flange Trial
Share the tool and flange drawing, cavity and vacuum keep-outs, tool material, release system, resin, bagging stack, cure profile, cleaning method, current buildup issue, replacement target, and part-quality checks. JIAO TAO TAO can help shortlist PTFE film, coated-fiberglass, or converted flange-strip constructions for controlled evaluation.
Discuss PTFE tape for composite tooling
Preventing Acetate Cloth Tape Edge Lift After Varnish Cure
Related Article

Need help choosing the right industrial tape?
Send us your application details, including temperature, surface material, size, quantity and current problem. Our team will help recommend a suitable tape material or custom die-cut solution.
simon@jiaotaotao.com
+86-136 1277 5969
+86-136 1277 5969
